-
First, Figure Out Which Situation You’re In
-
Scenario A: New Machine, Networked Control, and “What’s a Stepper Motor?”
-
Scenario B: Legacy Machine and the “Thomson Saginaw” Question
-
Scenario C: Bearing Swap – Self-Aligning Ball Bearing or Cylindrical Roller Bearing?
-
How to Tell Which Scenario You’re In
One question I get from our internal buyers is: “which one is cheaper?” My answer is usually the same: it depends on your situation. There is no universal winner between a stepper motor, a linear actuator, and a bearing replacement.
I’m a procurement manager at a mid-sized automation integrator. I’ve managed roughly $450k per year in motion-control components for the last six years, and I’ve logged every order in our ERP. What I’ve learned is that the cheapest PO is not always the cheapest installed part. Sometimes the higher-priced component saves you more money by the time it’s running.
First, Figure Out Which Situation You’re In
Here are the three situations I see most often, plus the “I’m new to this” version:
- Scenario A: You’re building a new machine with multiple axes and network control.
- Scenario B: You’re replacing a legacy actuator or ball screw on an older machine.
- Scenario C: You just need a bearing swap and you’re not sure if the cheaper bearing will survive.
If you’re still trying to understand the basics, start with Scenario A.
Scenario A: New Machine, Networked Control, and “What’s a Stepper Motor?”
A stepper motor is a brushless DC motor that moves in discrete steps. You command a certain number of steps, and the motor turns a fixed angle per step. No encoder is required for basic positioning. That’s why stepper motors are cheap and popular in open-loop systems. The catch is that torque drops off at higher speeds, and aggressive acceleration can cause missed steps.
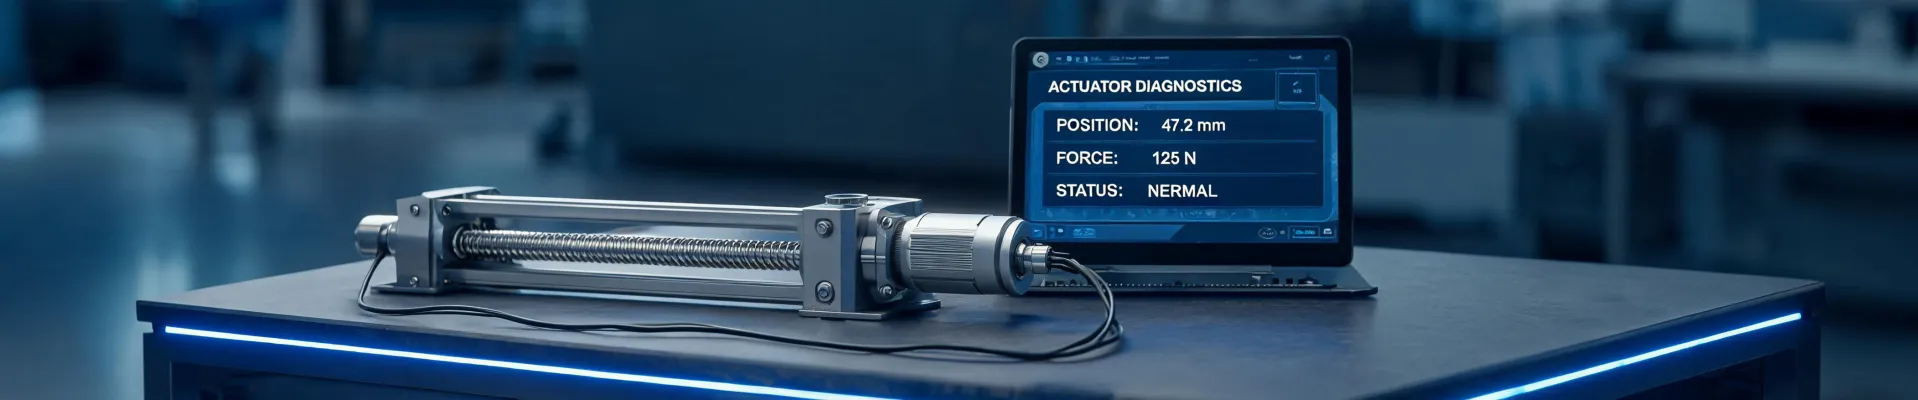
Now here’s the procurement decision that people mess up. If you’re building a machine with a PLC or IPC that already speaks CANopen, a Thomson linear actuator with CANopen CiA 402 can handle positioning and feedback in one component. The actuator follows the CiA 402 profile, which defines the controlword and statusword objects. In practical terms, the PLC can send a position command over the bus and see the actuator’s status in the same process. No separate step-and-direction wiring is needed.
I used to compare only the per-axis price. Then in Q2 2023, we switched from separate stepper drivers to integrated CANopen actuators on a three-axis station. Commissioning time dropped from five days to three. I don’t have a controlled study—just our timesheets—but the pattern held across four machines. The integrated actuator looked more expensive on paper, but the wiring, debugging, and PLC integration costs more than made up the difference.
So if you’re wondering “what’s a stepper motor, and should I use one?” here’s the honest answer: yes, if you have a simple machine with a dedicated controller, no bus communication, and no need for quick recipe changes. But if your machine has remote I/O, multi-axis coordination, or any kind of recipe management, a stepper with a stand-alone driver can be the wrong total cost. Not because it’s a bad motor, but because integration time is a cost too.
Scenario B: Legacy Machine and the “Thomson Saginaw” Question
Legacy replacement is a different animal. The phrase “Thomson Saginaw linear actuator” usually refers to the old Saginaw ball screw product lines that became part of Thomson. Those machines are still running in many plants, and finding the right replacement can be painful.
On the surface, a generic ball screw looks like half the price. I’ve made that mistake myself. We ordered a “will fit” screw for a packaging line, the lead time was fine, but the thread start difference and the end-machining tolerance created a racking problem. The rework and downtime cost us about 2.5 times the price of the OEM part. That was a hard lesson.
I still kick myself for not asking the right question first: is the line critical? For critical equipment, an OEM Thomson Saginaw replacement is the no-brainer. It might not be the cheapest line item, but it is the cheapest way to avoid an unplanned stop. A red flag for me is when a supplier quotes a replacement without asking about mounting dimensions, thread profile, and nut interface.
Take this with a grain of salt: if your machine is a prototype, or if you can absorb a week of downtime, a generic part can keep your budget under control. I’ve done that when the OEM part had a six-week lead time and the customer deadline was fixed. It comes down to the cost of being wrong. The machine doesn’t care what the label says; it cares about fit and tolerance.
Scenario C: Bearing Swap – Self-Aligning Ball Bearing or Cylindrical Roller Bearing?
Bearings are where the TCO mistake gets subtle. A self-aligning ball bearing looks like a special-purpose upgrade. It costs more than a standard bearing, and some buyers assume it’s automatically better. But its real advantage is that it can handle angular misalignment. If your shaft is subject to housing deflection or misalignment, the self-aligning ball bearing saves you the cost of precision-machined housings and repeated re-alignment.
A cylindrical roller bearing, on the other hand, is designed for higher radial load capacity and stiffness. It does not tolerate much misalignment. If your housing bores are true and the shaft is stiff, a cylindrical roller bearing is usually the better engineering choice. But if you install it on a shaft that wobbles, it will fail faster than the self-aligning option.
The question I hear more often than any other is “which bearing has the higher load rating?” The better question is “which bearing is correct for the actual load path and alignment of my machine?” A spec sheet rating does not mean it will survive your installation. I learned that when I ordered cylindrical roller bearings for a press with a worn housing. The bearings were fine. The housing was not. The rework cost more than the bearings themselves.
If you don’t know the housing roundness, measure it. A self-aligning ball bearing can mask a small amount of misalignment. A cylindrical roller bearing cannot.
How to Tell Which Scenario You’re In
Use this as a quick guide:
- If you’re building a new machine with a PLC that speaks CANopen and you need multi-axis coordination, a Thomson linear actuator with CANopen CiA 402 is worth the upfront cost.
- If you just need an inexpensive open-loop positioner on one simple axis, buy a stepper motor and a stand-alone driver. Just count the engineering and wiring time before you decide it’s cheaper.
- If you’re repairing a critical legacy machine, prioritize part certainty. A Thomson Saginaw linear actuator replacement may cost more than a generic, but the downtime cost can be far higher.
- If a bearing failed, measure the housing and shaft alignment before choosing. Then decide between a self-aligning ball bearing and a cylindrical roller bearing based on the real load path.
So what’s the bottom line? Unit price is the worst filter for motion control components. If your application needs network control, integration reliability, and minimal commissioning time, the higher-priced integrated option often wins. If you are maintaining legacy equipment, the “cheap” generic replacement can be the expensive one. And if you’re buying bearings, buy for the real misalignment, not the catalog rating.
Cost control is not about being cheap. It’s about making sure the money you spend is the money that keeps the machine running.